


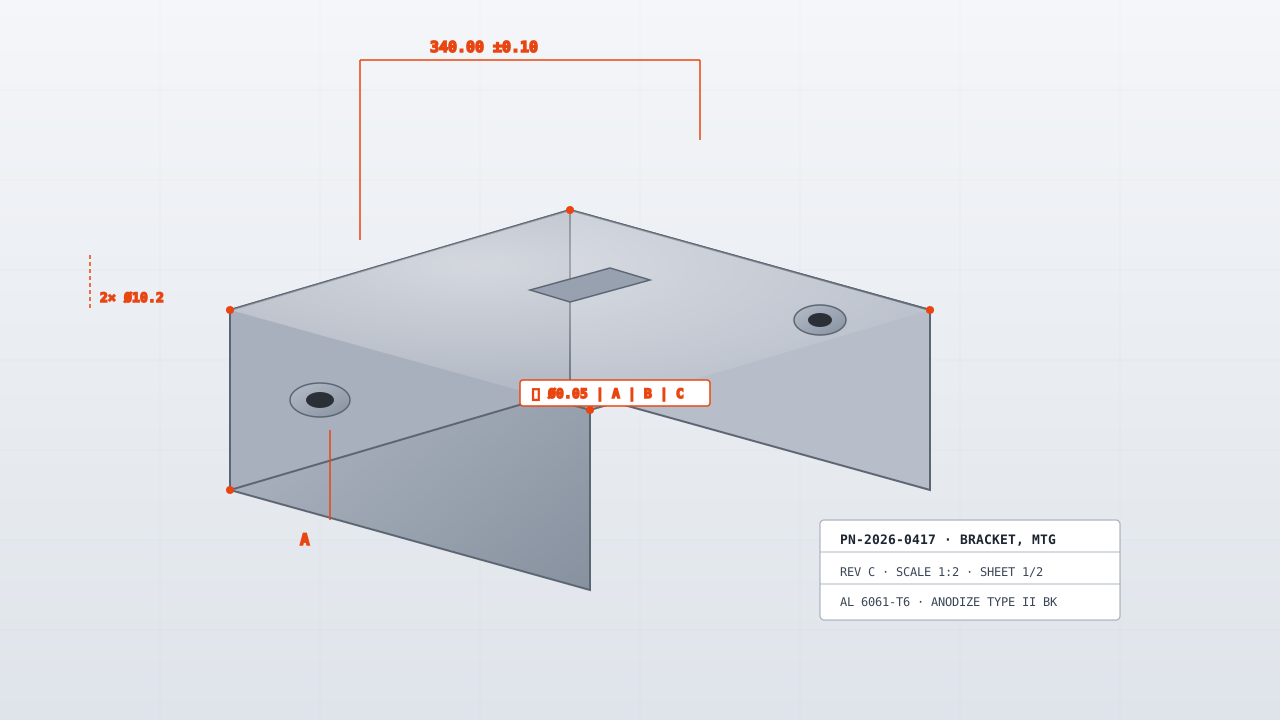
Cast Aluminium Brackets
Net-shape brackets cast in aluminium, consolidating a weldment into one part.
Brackets that would otherwise be fabricated from plate and tube. One casting replaces the cutting, welding, straightening and re-machining, and the rib pattern comes for free in the tool.
8–10 weeks
250 pieces
ISO 9001:2015 · IATF 16949
Technical Specifications
| Parameter | Value | Unit |
|---|---|---|
| Casting tolerance | DIN 1686 t5–t6 | - |
| Min wall | 2.5 | mm |
| Mounting face | ±0.05 | mm |
| Ribs | Cast, as designed | - |
| Max part weight | 12 | kg |
| Tooling lead time | 6–8 | weeks |
Available Materials
- A380 / ADC12
- AlSi10Mg
- LM25 (AlSi7Mg)
Typical Applications
- Suspension and mounting brackets
- Motor mounts
- Battery pack brackets
- Machine mounting feet
- Pump and tank brackets
Surface Finishes
- As-cast
- Shot blast
- Powder coat
- Anodise
- Machined mounting faces
Industries Served
- Automotive & EV
- Industrial Equipment
- Energy & Oil & Gas
- Agricultural Machinery
- Rail
What drives the price of this part
Derived from the callouts on this page. Where a driver is not on the drawing, it is not on this list.
- Tolerance
- Casting tolerance at DIN 1686 t5–t6 is the tightest callout this family carries. Tightening a callout is a process decision, not a machining decision: below the standard ±0.005 mm the work moves to grinding or jig boring, and the price moves with it.
- Part size
- Min wall at 2.5 mm decides which machine the part lands on and how many setups it needs. Size is the driver buyers most often leave out of a first enquiry, and it is the one that changes the quote fastest.
- Order size
- Minimum order is 250 pieces, where setup and tooling are amortised across the batch and per-part cost settles around cycle time and material. Below that quantity the same part costs more per piece, not less.
See how cycle time is calculated in the machining time calculator and what else moves a price in the cost driver reference.
How these parts are inspected
Matched to the callouts above and the instruments actually on the floor.
- Coordinate measuring machine (Zeiss CONTURA G2, two machines, GR&R 8.4% on the critical feature)
- Dimensional report against the drawing, with a 100% check on critical features rather than a sample
- Certificate of conformance and the mill certificate with every shipment
- First article inspection to AS9102, because this family carries an aerospace or automotive certificate
The full equipment list, with counts, is on the capability page; the inspection sequence is on quality and inspection.
Questions buyers ask
- When does casting beat a weldment?
- Above a few hundred a year, or when the welded version needs straightening after welding. Casting also gives you ribs and bosses that a fabrication cannot produce without extra parts.
- How much machining does a cast bracket need?
- Usually only the mounting and bearing faces - everything else stays as cast. We build the machining fixture together with the tool so the faces locate off the casting itself.
Related part families
Aluminium Die Cast Housings
High-pressure aluminium housings from 0.5–15 kg, trimmed, machined and sealed-face checked in-house.
Welded Frames & Structures
TIG and MIG welded steel frames, squared on a fixture and stress-relieved before machining.
Gravity Die Castings
Gravity cast aluminium parts with lower porosity, for pressure-tight and machined-heavy work.