

Quality & Inspection
ISO 9001:2015 · AS9100D · IATF 16949 · NADCAP. Two Zeiss CMMs on the shop floor. First-pass yield above 96%, measured and reported per order.
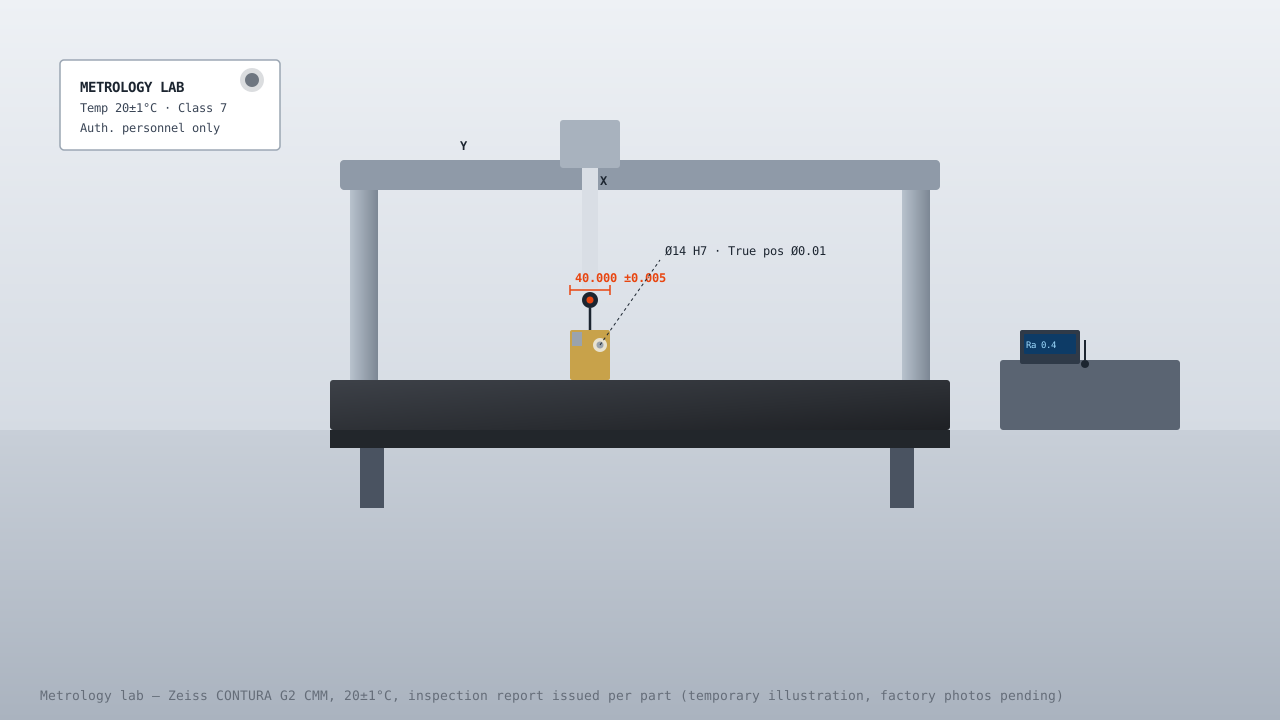
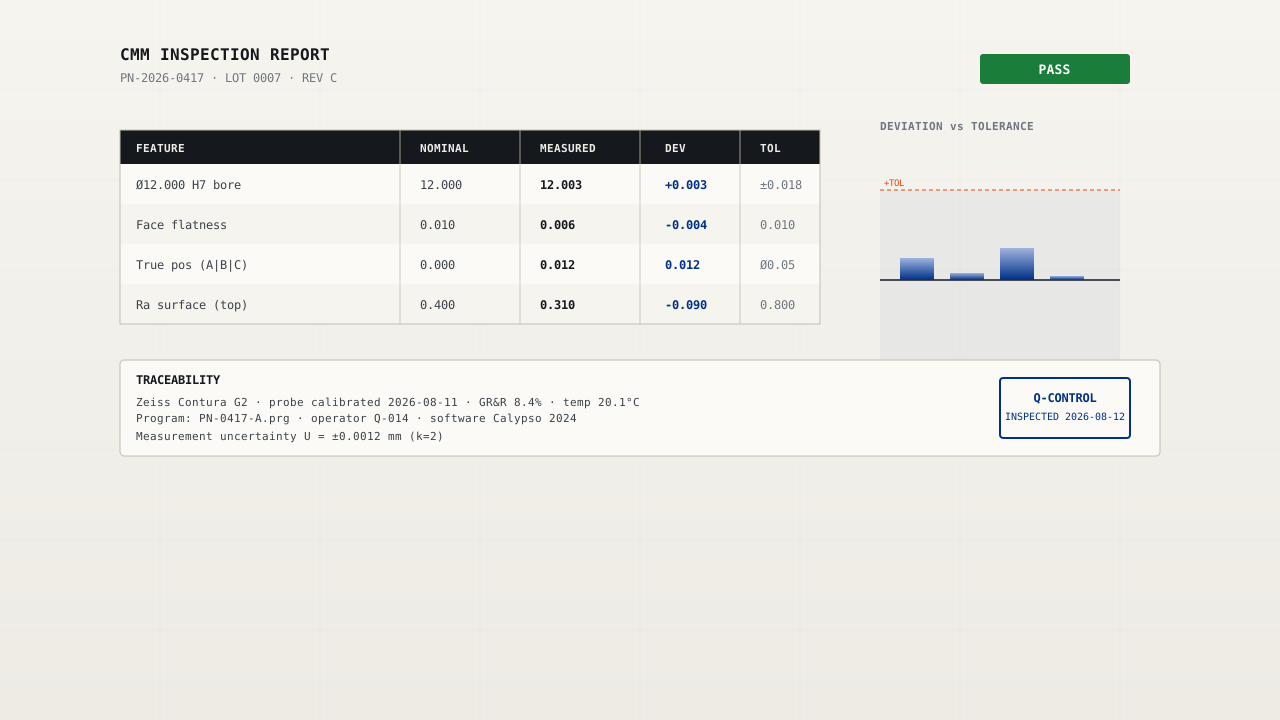
CMM REPORT · NOMINAL / MEASURED / DEV · PASS
Every critical feature measured. Report ships with the lot.
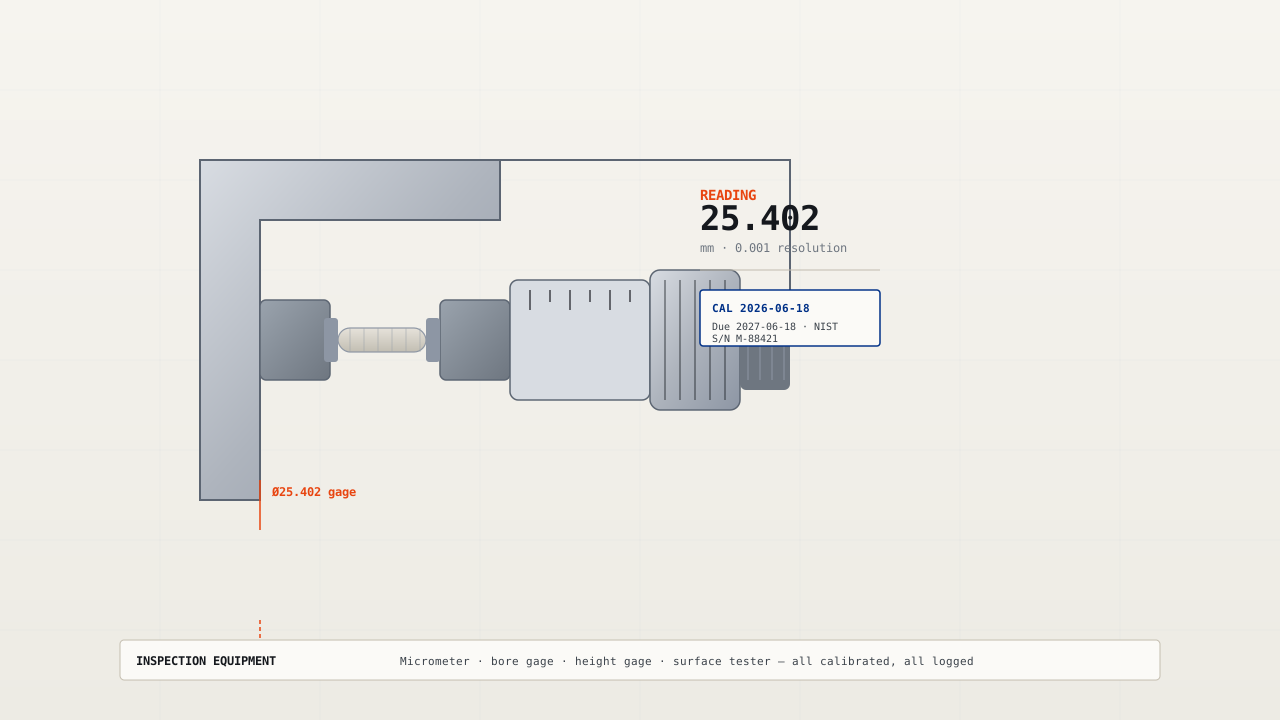
CALIBRATED INSTRUMENTS · 0.001 MM
Micrometers, bore gages, height gages - NIST-traceable, on schedule.
How a Part Gets Inspected
Design Review & DFM
Engineer reviews your CAD for manufacturability, tolerance stack-ups, and cost-saving opportunities before quoting. FMEA completed for critical features.
First Article Inspection (FAI)
First part off the machine goes to the CMM lab. Full dimensional report per AS9102. Customer sign-off required before production release.
In-Process Inspection
SPC monitoring at every critical operation. CMM checks at defined intervals. Material certification verification. Surface finish measurement.
Final Inspection & Shipment
100% dimensional check on critical features. CoC, material certs, CMM reports packed with shipment. ISO 9001:2015 documentation control.
Certifications & Scope
ISO 9001:2015
Bureau Veritas
Design, manufacture and inspection of precision machined components
BV-2015-18452
Request a copy →AS9100D
PRI Registrar
Aerospace quality management for safety-critical component production
PRI-AS9100-2024-7831
Request a copy →IATF 16949
TUV SUD
Automotive quality management for serial production parts
TS-16949-2024-4521
Request a copy →NADCAP (NDT)
PRI
Non-destructive testing: penetrant, magnetic particle, ultrasonic
NADCAP-2024-3317
Request a copy →NADCAP (HT)
PRI
Heat treatment: annealing, solution treat, age harden
NADCAP-HT-2024-2145
Request a copy →Certifications verified by Bureau Veritas, PRI Registrar, and TUV SUD. Copies available upon request in full resolution.
Inspection and support equipment
| Function | Equipment | Qty | What it changes for the part |
|---|---|---|---|
| Metrology | Coordinate measuring machineZeiss CONTURA G2 | 2 | Dimensional reports against the drawing, GR&R 8.4% on the critical feature |
| Metrology | Optical comparatorProfile projection | 1 | Edge, radius and thread-form checks that are faster on a screen than on a CMM |
| Metrology | Surface roughness testerMitutoyo | 1 | Verifies the Ra called out on the drawing instead of assuming it from the insert |
| Metrology | Rockwell hardness testerRockwell C | 1 | Confirms heat-treat results on the part, not on the certificate alone |
| Metrology | Hand gaugesMicrometers · bore gauges · thread gauges | 1 | Shop-floor checks between CMM runs, which is what keeps a batch inside tolerance |
| Support | Ultrasonic wash stationAqueous | 1 | Removes coolant and swarf before inspection so a measurement is not taken through a film |
| Support | Vibratory finisher and deburring benchesCeramic media | 1 | Edge break and surface prep before finishing |
| Support | Heat treat ovensIn-house | 1 | Stress relief and through-hardening without sending the lot out |
| Support | Shot blast cabinetDry blast | 1 | Uniform matte finish and surface preparation before coating |
| Support | Laser markingEngraving | 1 | Part numbers and lot codes marked permanently, readable after plating |
Counts are per model as installed.
Material Traceability
- Full material certification per EN 10204 Type 3.1
- Heat/lot number tracking through every process step
- Certifications verified against material standards (ASTM, AMS, QQ, MIL)
- Certificate of Conformance with each shipment
- RoHS / REACH compliance declarations available
- Conflict minerals statement upon request
FAI / PPAP Capability
- AS9102 First Article Inspection (aerospace/defence)
- PPAP Level 3 documentation (automotive)
- Gauge R&R studies per MSA 4th edition
- Process FMEA per AIAG/VDA handbook
- Control plan generation with customer-specific requirements
- APQP documentation support for new product launches
What a CMM Report Looks Like
This is the dimensional report that ships with a typical order. Feature names, nominals and measured values - no interpretation needed, your QA files it as-is. (Sample data, customer name removed.)
| Feature | Nominal | Measured | Deviation | Tolerance | Status |
|---|---|---|---|---|---|
| Ø12 H7 bore | 12.000 | 12.003 | +0.003 | +0.018 / 0 | PASS |
| Bore true position (A|B) | Ø0.02 | Ø0.011 | - | Ø0.02 max | PASS |
| Face flatness | 0.01 | 0.006 | - | 0.01 max | PASS |
| Overall length | 420.000 | 419.997 | -0.003 | ±0.05 | PASS |
| Surface finish Ra | 0.8 | 0.62 | - | 0.8 max | PASS |
Machine: Zeiss CONTURA G2 · Temperature 20±1°C · Report ID: CMM-2026-0715-034
PPAP Level 3 - What We Deliver
Customer-specific requirements (CSR) reviewed before quoting - if your OEM expects additional items, we add them to the plan up front.
Verified Claims - What We State, and What Proves It
Every claim on this site is classified by how it is evidenced - certified, accredited, capable, or internal practice. Nothing is presented as certified unless a certificate exists. Unverified claims are flagged for human review. The four certificate claims are not repeated here: they are listed above with issuer, scope and certificate number.
| Claim | Type | Evidence | Source | Verified |
|---|---|---|---|---|
| 98.7% on-time delivery | INTERNAL_PRACTICE | ERP order fulfilment records, last 12 months | Internal ERP (order tracking) | 2026-06-01 |
| 12,500+ projects delivered since 2005 | INTERNAL_PRACTICE | Project ledger count since founding | Internal ERP / project records | 2026-06-01 |
| In-house CMM metrology - two Zeiss machines, GR&R 8.4% | INTERNAL_PRACTICE | GR&R study on critical feature, 2026-06-18 | Internal metrology lab records | 2026-06-18 |
| ±0.005mm standard machining tolerance | CAPABLE | Process capability studies on standard features; tighter on request | Internal process data / CMM records | 2026-06-01 |
| 5-axis machining on DMG MORI / Mazak centres | CAPABLE | Machine fleet list; 40+ CNC machines on the shop floor | Internal equipment register | 2026-06-01 |
| ITAR-compliant handling of export-controlled data | INTERNAL_PRACTICE | Data-handling procedure for controlled drawings; written procedure on request | Internal compliance procedure | 2026-06-01 |
| Weekly FedEx / DHL shipping to US, EU and Middle East | INTERNAL_PRACTICE | Carrier booking records, 15 countries served | Internal logistics records | 2026-06-01 |
Last verified 2026-06-18 · certificate copies and audit kit available below · 1 item flagged for human review
SPC & Cp/Cpk - Process Evidence
For serial production we do not only check the part - we watch the process. Statistical process control tells you whether a run is drifting before it leaves tolerance, and capability indices tell you how much headroom the process actually has.
SPC
X-bar & R charts
Critical dimensions charted per batch; out-of-control points investigated before shipment, not after.
Cp / Cpk
≥ 1.33 typical
Capability reported on request for serial features. If a process cannot hold 1.33 with margin, we tell you before quoting.
GR&R
8.4% on critical feature
Gauge repeatability & reproducibility study on the CMM, 2026-06-18. Measurement system is not the bottleneck.
Digital Trust Center - Audit Kit
We cannot bring your quality team to Xi\u2019an every quarter, so we bring the audit to you. Request the full kit below - no sales call required, nothing gated behind a meeting:
ITAR & Export Control
ITAR-compliant data handling for defence work. Defence data on physically isolated servers, access restricted to trained staff, transfers logged.
Calibration System
All inspection equipment calibrated per ISO 10012. Zeiss CMM serviced annually. Gauges certified to NIST-traceable standards. Recall system prevents use of uncalibrated tools.
Supplier Audit Welcome
On-site quality audits welcomed. Remote audits supported via video walkthrough. Quality manual and procedures available for review upon request.
Documentation Included with Every Order
Certificate of Conformance (CoC)
PDFMaterial Certification (EN 10204 3.1)
PDFDimensional Inspection Report (CMM)
PDFSurface Finish Measurement Report
PDFSee also: Tolerance Guide · Surface Finishes Guide · IP Protection Policy
Put the inspection data to work on your part.
Send the drawing. You get CMM-backed quality and a report with every shipment - not a promise.