


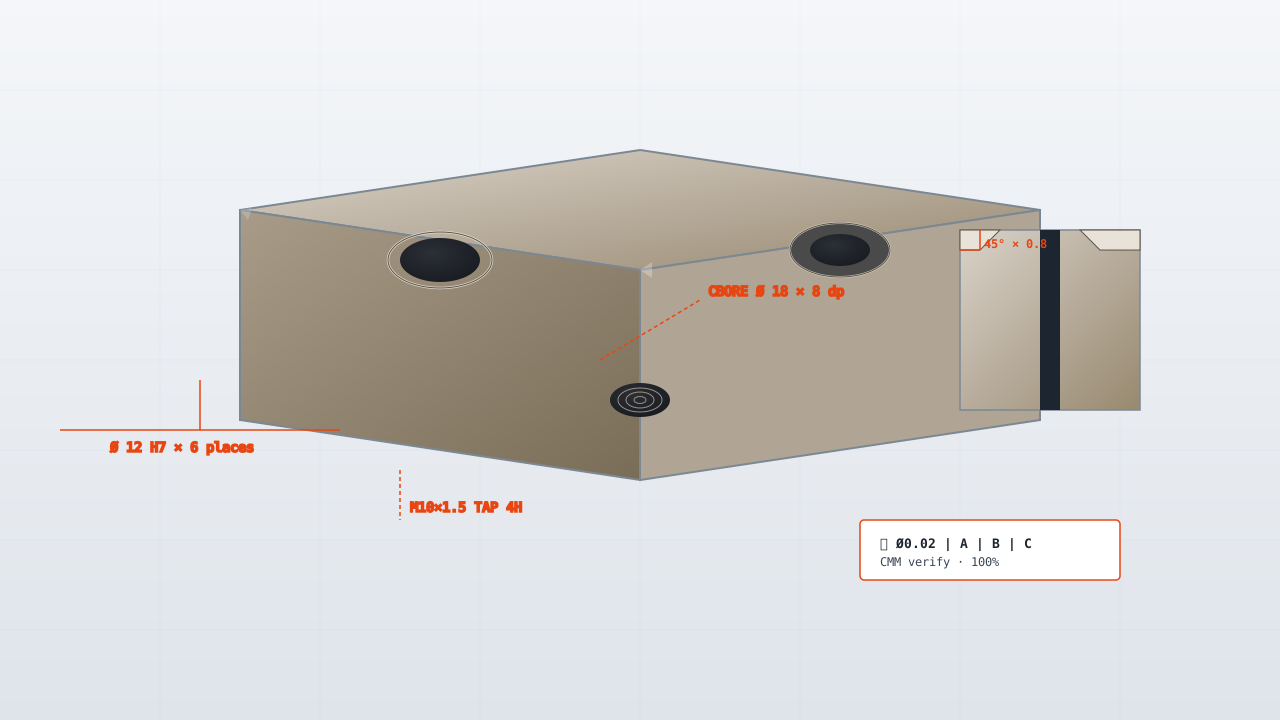
Split Bushings & Half Bearings
Two-piece bushings and half shells for shafts that cannot be withdrawn.
Split bushings for crankshafts, long shafts and anything that stays in place during a rebuild. The halves are made as a pair so the joint line closes without a step.
4–6 weeks
2 pieces
ISO 9001:2015
Technical Specifications
| Parameter | Value | Unit |
|---|---|---|
| Bore range | Ø20–Ø600 | mm |
| Joint face flatness | 0.01 | mm |
| Bore tolerance | H7 / H8 | - |
| Wall thickness | 3–30 | mm |
| Lining | Solid or babbitt | - |
| Pair matching | Made as a set | standard |
Available Materials
- Bronze C932
- Aluminium bronze C954
- Babbitt-lined steel
- PTFE-lined steel
- Cast iron
Typical Applications
- Crankshaft main bearings
- Line shaft bearings
- Conveyor and mill trunnions
- Marine stern tubes
- Pump shafts
Surface Finishes
- Machined joint faces
- Babbitt lined
- Lubricated (graphite / oil holes)
- Ground IDs
Industries Served
- Energy & Oil & Gas
- Marine
- Mining & Construction
- Water Treatment
- Industrial Equipment
What drives the price of this part
Derived from the callouts on this page. Where a driver is not on the drawing, it is not on this list.
- Tolerance
- Joint face flatness at 0.01 mm is the tightest callout this family carries. Tightening a callout is a process decision, not a machining decision: below the standard ±0.005 mm the work moves to grinding or jig boring, and the price moves with it.
- Part size
- Bore range at Ø20–Ø600 mm decides which machine the part lands on and how many setups it needs. Size is the driver buyers most often leave out of a first enquiry, and it is the one that changes the quote fastest.
- Order size
- Minimum order is 2 pieces, so on a first order setup and programming are spread over very few parts and they are most of the price. Repeat orders at the same quantity are cheaper without anything on the drawing changing.
See how cycle time is calculated in the machining time calculator and what else moves a price in the cost driver reference.
How these parts are inspected
Matched to the callouts above and the instruments actually on the floor.
- Coordinate measuring machine (Zeiss CONTURA G2, two machines, GR&R 8.4% on the critical feature)
- Dimensional report against the drawing, with a 100% check on critical features rather than a sample
- Certificate of conformance and the mill certificate with every shipment
- Bore gauges and an optical comparator for hole position and edge form
The full equipment list, with counts, is on the capability page; the inspection sequence is on quality and inspection.
Questions buyers ask
- Why must split bushings be made as a pair?
- Because the two halves are machined together so the joint closes without a step. Mix halves from different sets and the shaft rides over a ridge twice per revolution.
Related part families
Sintered Bronze Bushings
Oil-impregnated bronze bushings with controlled porosity, for places you cannot re-lubricate.
Composite & PTFE Bushings
Dry-running composite bushings for dirty, washdown or unlubricated service.
CNC Machined Bushings
Machined bushings, sleeves and spacers with bored IDs held to H7, flanged on request.