

Sheet Metal Brackets
Laser cut and press-brake formed brackets, 0.5–6 mm, with rivet nuts and inserts fitted in-house.
Brackets cut on a fibre laser and formed on CNC press brakes with bend-angle compensation, so the 90° is 90°. Hardware is pressed in here rather than sent out, which keeps the hole-to-edge distances inside ±0.1 mm.
2–3 weeks
10 pieces
ISO 9001:2015 · IATF 16949
Technical Specifications
| Parameter | Value | Unit |
|---|---|---|
| Bend tolerance | ±0.1 | mm |
| Bend angle | ±0.5 | ° |
| Sheet thickness | 0.5–6.0 | mm |
| Max bend length | 3,000 | mm |
| Laser cut edge | ±0.05 | mm |
| Holes from | Ø1.0 | mm |
Available Materials
- Mild steel DC01
- Galvanised steel DX51D
- Stainless 304
- Stainless 316L
- Aluminium 5052
- Aluminium 6082-T6
Typical Applications
- Control cabinet mounting
- Machine guards and covers
- Battery pack frames
- Cable management trays
- Structural tie plates
Surface Finishes
- Powder coat (any RAL)
- Zinc plating
- Hot-dip galvanising
- Anodise
- Passivate
- As-formed
Industries Served
- Automotive & EV
- Industrial Equipment
- Energy & Oil & Gas
- Telecom & 5G
- Rail
What drives the price of this part
Derived from the callouts on this page. Where a driver is not on the drawing, it is not on this list.
- Tolerance
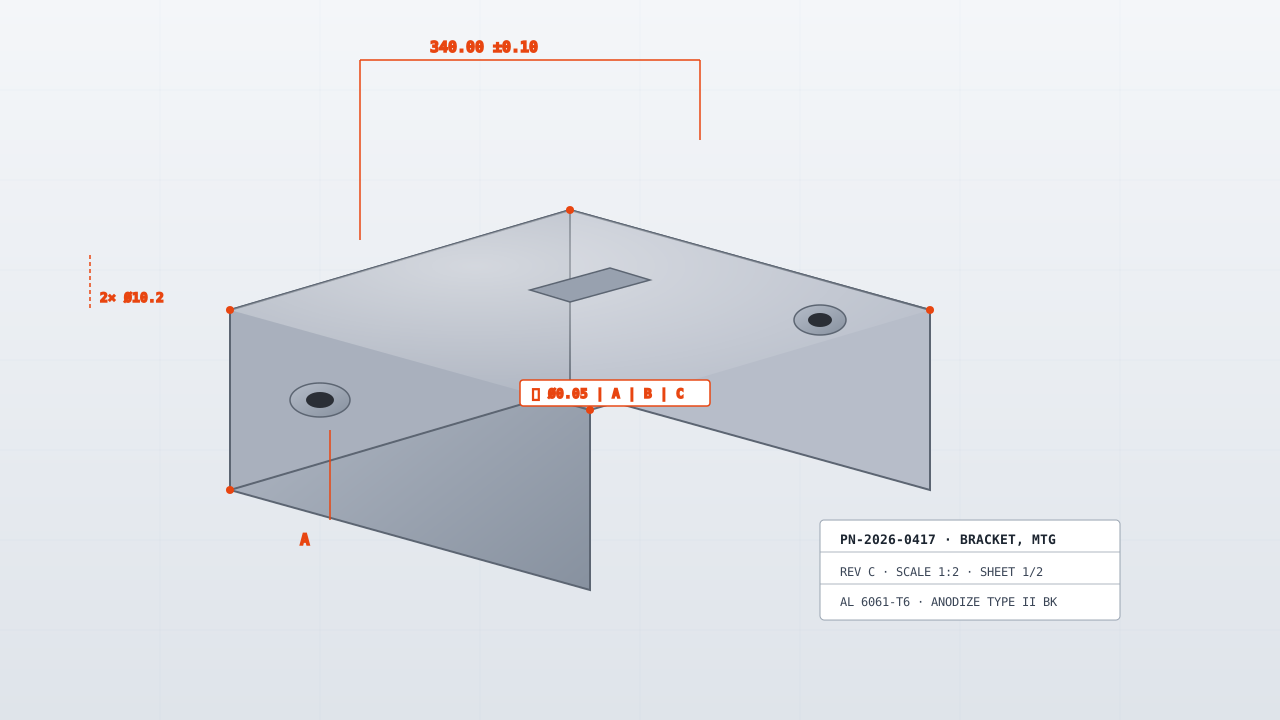
- Bend tolerance at ±0.1 mm is the tightest callout this family carries. Tightening a callout is a process decision, not a machining decision: below the standard ±0.005 mm the work moves to grinding or jig boring, and the price moves with it.
- Part size
- Sheet thickness at 0.5–6.0 mm decides which machine the part lands on and how many setups it needs. Size is the driver buyers most often leave out of a first enquiry, and it is the one that changes the quote fastest.
- Material
- The first material listed, Stainless Steel 304 / 304L, rates 4/10 on our machinability scale at 201 HB. On this shop's scale a harder alloy means slower passes and more tool changes, and that is cycle time the quote has to carry.
- Order size
- Minimum order is 10 pieces, so on a first order setup and programming are spread over very few parts and they are most of the price. Repeat orders at the same quantity are cheaper without anything on the drawing changing.
See how cycle time is calculated in the machining time calculator and what else moves a price in the cost driver reference.
How these parts are inspected
Matched to the callouts above and the instruments actually on the floor.
- Coordinate measuring machine (Zeiss CONTURA G2, two machines, GR&R 8.4% on the critical feature)
- Dimensional report against the drawing, with a 100% check on critical features rather than a sample
- Certificate of conformance and the mill certificate with every shipment
- Bore gauges and an optical comparator for hole position and edge form
- First article inspection to AS9102, because this family carries an aerospace or automotive certificate
The full equipment list, with counts, is on the capability page; the inspection sequence is on quality and inspection.
Questions buyers ask
- What is the minimum flange for a bend?
- Four times the material thickness, plus the die width. Under that the press brake cannot form the bend without the punch bottoming out on the flange, so we will flatten it to fit a smaller die and tell you before cutting.
- Do you fit rivet nuts and press studs?
- Yes, in-house before finishing. Fit them after powder coating and you chip the coating around every hole, which is where the rust starts.
Related part families
Precision Chassis & Enclosures
EMI-shielded enclosures and instrument chassis, formed and welded to ±0.1 mm with gasket channels.
Welded Frames & Structures
TIG and MIG welded steel frames, squared on a fixture and stress-relieved before machining.
Assembled Sub-Assemblies
Machined, plated, inspected and kitted as one part number, with the tolerance stack-up owned in one place.